GX MAGNET Logo

Permanent-Magnet Rotor Assemblies

Motor Rotor Assembly
Manufacturer

GX Magnet has years of in-depth experience manufacturing permanent-magnet rotor assemblies. Our product portfolio covers a wide range of motor rotors, with custom manufacturing available per customer drawings. Every project is developed with consideration of operating principle, magnet topology, pole layout, shaft interface, retention method, rotational speed and acceptance requirements.

  • Over 2,500 custom motor rotors developed for clients
  • Magnet system, rotor core, shaft, retention, runout and balance reviewed together
  • Offer custom prototype sampling complying with clients’ drawings and technical standards.
Supply statement: drawing-defined permanent-magnet rotor assemblies and approved rotor subassemblies
Permanent-magnet rotor assemblies for motors and generators
Bosch logo
Midea logo
Siemens logo
WEG logo
Gree logo
Shimge logo
Copreci logo
Buhler logo
Samsung logo
Nidec logo

Project screening

What Buyers Should Confirm Before Selecting a Rotor Route

A useful review starts with the machine operating principle, then defines the magnet system, mechanical interfaces and finished-assembly acceptance criteria.

Machine type
PMSM, BLDC, PM stepper, PM generator
Rotor configuration
SPM, IPM, ring, segmented, inner-rotor or outer-rotor design
Functional requirements
Pole layout, waveform, speed, runout, retention and balance
Required input
Assembly drawing, BOM, mating stator, environment and annual demand

Rotor types by operating principle

We supply matching rotor assemblies according to your requirements

Permanent-magnet rotors may share similar components, but their pole layout, magnetic waveform, mechanical structure and validation requirements depend on how the machine produces torque or electrical power.

One Partner, End-to-End Coordination

From Magnetic Powder to Rotor Assembly

GX is more than a magnet supplier. We deliver complete permanent-magnet rotor assemblies ready for installation.

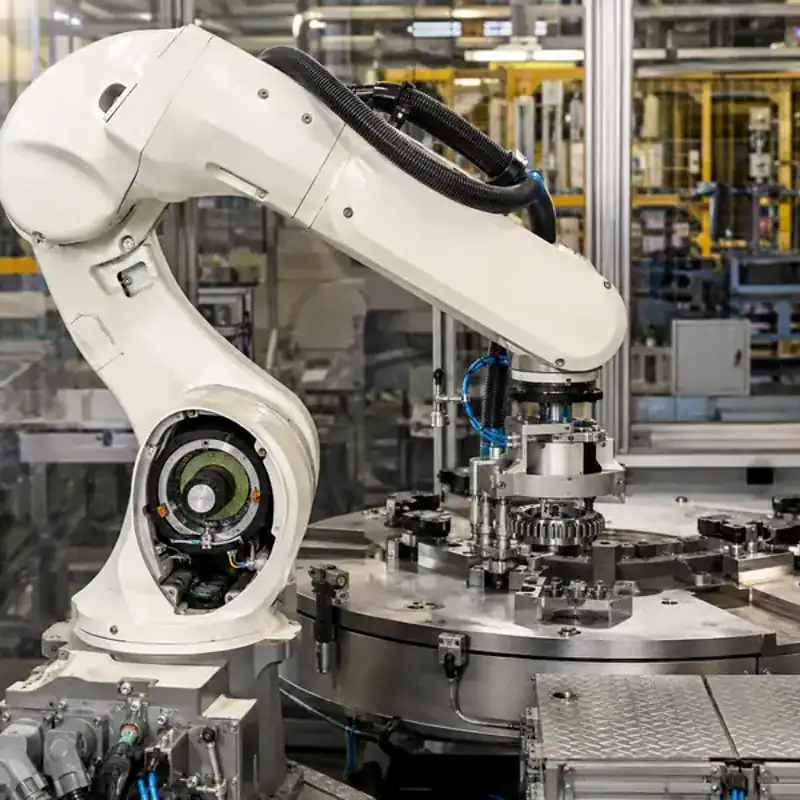
Our integrated manufacturing resources cover the full process—from magnetic powder preparation, compaction, sintering, precision grinding and multipole magnetization to rotor assembly with automated adhesive dispensing, robotic magnet placement, servo press-fitting and in-line magnetic flux inspection.

This means fewer supplier interfaces, tighter process control and a shorter path from customer drawing to volume production.

Drawing-defined permanent-magnet rotor components and interfaces
Magnet systemSintered ferrite multipole rings and arc-segment magnets — for cost-sensitive fan and pump motors  
Injection-molded bonded ferrite rotors — for high-volume household appliances and automotive sensors  
Injection-molded bonded NdFeB rotors — for compact motors with limited space and higher magnetic-flux requirements  
Sintered NdFeB SPM rotors — for medium- to high-power, high-performance drive motors
One drawing, one purchase order and one point of responsibility. GX coordinates the material and manufacturing route around your performance targets and cost requirements—not the other way around.
Precision Multipole MagnetizationUniform pole distribution directly affects torque ripple and operating noise.
GX supports magnetization patterns from 2 to more than 32 poles, with diametrical, axial and radial configurations. Precision magnetizing fixtures control pole-angle deviation within ±0.5° and pole-to-pole flux variation within ±2%, subject to the agreed product geometry and inspection method.
Every rotor undergoes 100% magnetic flux inspection before release. Nonconforming parts are stopped at the magnetization station instead of reaching the customer’s test bench.
Assembly Accuracy and Quality ControlRotor assembly accuracy affects motor performance, especially at high speed. Poor concentricity, uneven adhesive thickness or insufficient magnet retention can lead to vibration, noise and premature failure.
GX controls each assembly step: CCD vision guides magnet placement to a position tolerance of ±0.05 mm; automated dispensing helps maintain a consistent adhesive layer; rotor-bore-to-shaft concentricity is controlled to ≤0.02 mm; and dynamic balancing is performed to grade G2.5. Pull-off force testing checks magnet retention against the agreed acceptance criteria.
Every rotor assembly receives final inspection before shipment, so customers receive a finished unit ready for installation.
Design for Manufacturability (DFM) SupportGX gets involved early in rotor design, rather than waiting for a finalized drawing before quoting. Before tooling begins, our engineering team reviews magnet geometry, tolerance stack-up and production feasibility to identify cost savings without compromising the required performance.
Could several magnet segments be replaced with a single molded part? Can an unnecessarily tight tolerance be relaxed? Can the proposed shape be produced at a practical yield? We address these questions before they become production problems.
The goal is a rotor design that costs less to make, is easier to assemble and is ready for a smooth transition from first-article approval to volume production.

Engineering review

Permanent-Magnet Rotor Assembly Review Parameters

Based on the customer’s drawings, proposed design and intended application, GX Magnet evaluate feasibility and recommend an appropriate solution.

ParameterSpecification / Review Basis
Machine TypePMSM, BLDC motor, permanent-magnet stepper motor, permanent-magnet generator.
Rotor TopologySPM, IPM, multipole ring, segmented-magnet, inner-rotor, outer-rotor or drawing-defined flux-barrier structure.
Magnet SystemMagnet material, grade, dimensions, coating, magnetization direction, pole count and approved pole map.
Electromagnetic TargetMagnetic flux, surface flux-density waveform, back-EMF target or another functional characteristic measured under agreed conditions.
Mechanical InterfacesRotor OD, stack length, shaft or hub interface, bearing seats, torque-transfer features, fits and functional datums.
Retention and RotationAdhesive, interference fit, mechanical lock, sleeve or molded interface, together with rated speed, overspeed condition, TIR and balance requirements.
Environment and ValidationOperating temperature, duty cycle, fluid or moisture exposure, vibration, sample approval and required inspection records.

Final dimensions, tolerances, magnetic acceptance criteria and rotational limits follow the approved project drawing and validation plan; they are not common limits for every rotor type.

GX Magnet review of permanent-magnet rotor projects with OEM buyers

Project communication

Review the Rotor Route Before Formal Quotation

Custom magnetic rotors do not have a standard price. To avoid quoting against incomplete information—and later price revisions or delays—our engineers review the application, drawings and delivery requirements before preparing a formal quotation. GX can usually align these details in a single phone or video call.

Application and Technical Requirements

GX first confirm the motor type and end use, such as a pump, fan, compressor, household appliance, power tool or automotive system. We also review operating speed, duty cycle, temperature and environment, along with the magnet grade and required magnetic performance, rotor design (surface-mounted, interior or multipole ring), air gap, balance grade and inspection criteria.

Drawing Review and Design Recommendations

GX review the rotor or assembly drawings for dimensions, tolerances, fits and compatibility with the mating shaft and stator. Our engineers can then recommend changes to the material, magnetization, process or structure to improve performance and manufacturability—and reduce cost where feasible.

Annual Volume and Delivery

GX confirm the estimated annual demand, order quantities and schedule from samples through volume production. This helps us plan volume-based pricing, tooling and lead times. We also agree on the supply scope—magnetic components only or a finished rotor assembly—plus packaging, shipping method (courier, air or sea freight), trade terms and destination.

ROTOR ASSEMBLY CONTROL

From Loose Magnets to Assembled Rotor Cores

GX supplies more than individual magnets. We install magnet segments into rotor cores using drawing-defined pole positions and assembly datums. CCD vision positioning, controlled adhesive dispensing, servo-assisted insertion and in-process inspection help carry the approved assembly method from samples into repeat production.

Permanent-magnet rotor assembly review and production process
01

Accurate Magnet Placement

Each segment is positioned to the specified pole sequence and circumferential location. The assembled magnetic surface is checked against the rotor’s reference datum to control runout and support a consistent working air gap.

02

Secure Magnet Retention

Adhesive quantity, application position, bond line and curing are controlled during assembly. Where the design requires it, mechanical retention or a sleeve is incorporated to address the loads imposed by operating speed.

03

Balance the Assembled Rotor

Installing magnets changes the rotor’s mass distribution. When dynamic balancing is included in the supply scope, it is performed on the assembled rotor—not inferred from the balance of the bare core. The required grade, such as G2.5 or G6.3, follows the customer’s drawing and operating conditions.

04

Repeatable Volume Assembly

Dedicated fixtures, controlled machine settings and in-process checks reduce reliance on manual magnet placement. Pole position, runout, magnetic output and retention are inspected to the agreed criteria so that production units follow the approved sample.

Verification

Inspection Connects Rotor Geometry to Functional Output

Inspection follows the approved BOM and drawing across incoming components, assembly interfaces, magnetic results, runout, retention and balance.

Inspection and validation for permanent-magnet rotor assemblies
Inspection item Control approach Benefit to the customer
Magnetic performance Use a fluxmeter, Helmholtz coils and a gaussmeter to conduct 100% inspection of total rotor flux, surface flux density at each pole, polarity, pole count and magnetic flux density waveform. Measure demagnetization curves on batch samples to verify Br, Hcj and (BH)max against the specified grade and temperature rating. Keep magnetic flux within its nominal tolerance. Ensures the motor meets its torque, back-EMF and efficiency targets, prevents polarity errors, maintains consistent performance across batches and resists demagnetization during long-term high-temperature operation.
Dimensions and geometric tolerances Use calipers, micrometers, optical measuring systems, coordinate measuring machines and runout gauges to perform 100% inspection of critical dimensions, outer-diameter radial runout, coaxiality, roundness and shaft fits against the drawing tolerances. Ensures the rotor fits and assembles correctly, maintains a uniform air gap, and prevents eccentricity and rotor-to-stator contact. It also helps reduce vibration, noise and uneven bearing wear.
Dynamic balance Balance every rotor using single-plane or two-plane correction and material removal as required. Control residual unbalance to grade G2.5 for high-speed or precision applications, or G6.3 for general applications. Reduces vibration and high-pitched noise at speed, protects bearings, seals and couplings, and helps extend motor service life.
Mechanical reliability and safety and safetyInspect magnet retention and the integrity of sleeves or overmolded structures. Perform overspeed testing at approximately 1.2 times rated speed, along with press-fit, torque-resistance and pull-off force tests. For NdFeB components, measure coating thickness, conduct salt spray testing, and check for cracks, chipped edges and porosity. Ensures magnets remain secure at high speed, prevents slipping or detachment during repeated starts and stops, and protects against corrosion in damp environments.
Material compliance, traceability and packaging Provide material certificates or Certificates of Conformity (CoC) for each batch, together with RoHS/REACH compliance documentation. Package magnetized or unmagnetized rotors with appropriate magnetic shielding and protection against moisture and impact. Provides material traceability and audit records, supports export and automotive quality requirements, and helps ensure safe transport without attracting iron particles while meeting air-freight requirements.

Export Packaging & International Delivery

A permanent-magnet rotor assembly needs more than a strong outer carton. Magnetized parts may require air-freight magnetic-field assessment, while shafts, bearing seats, coatings and installed magnets need protection from movement, moisture and impact. GX Magnet’s magnetic products have been exported to more than 20 countries. For rotor assemblies, we confirm the packing method against the actual part and shipping route.

Magnetic-Field Control for Air Freight

For magnetized rotors shipped by air, the external field is assessed on the completed package, not the unpacked rotor alone. Pole arrangement, spacing or shielding can be adjusted where needed. GX coordinates the applicable measurement, marking and documentation requirements with the freight provider before dispatch; acceptance depends on the package and the carrier’s current requirements.

Moisture and Corrosion Protection

For longer shipments, the packing plan considers the magnet coating, exposed steel surfaces and the possibility of condensation. Moisture-barrier materials and desiccants can be used where appropriate, while shafts and bearing seats receive protection suited to their surface condition. Packing materials are selected so they do not damage coatings or interfere with subsequent assembly.

Protection of Precision Interfaces

Rotors are individually located within the inner packaging to prevent rolling, part-to-part contact and loading on the shaft ends. Protective covers or separators can be added for bearing seats, magnet faces and other drawing-defined critical surfaces. The outer package is selected according to rotor weight, quantity and the handling expected along the route.

Documents Matched to the Shipment

Commercial invoices, packing lists and package identification are prepared against the confirmed order. Certificates of origin, inspection records or magnetic-field assessment documents can be arranged when required by the customer, destination or carrier. The required document set is confirmed before shipment rather than treated as identical for every rotor order.

Delivery Terms Confirmed Up Front

GX can coordinate with a customer-nominated forwarder or discuss express, air and sea-freight options. The quotation defines the delivery term, shipping point, packing scope, freight and insurance responsibilities, and required documents. Transit estimates are provided for the specific destination and route; they are not presented as a fixed worldwide delivery time.

Application Fit

Permanent-Magnet Rotor Applications

GX Magnet supplies permanent-magnet rotor assemblies for four main application areas. Each has different performance requirements, material preferences and operating conditions. Our material options and assembly capabilities cover this range of needs.

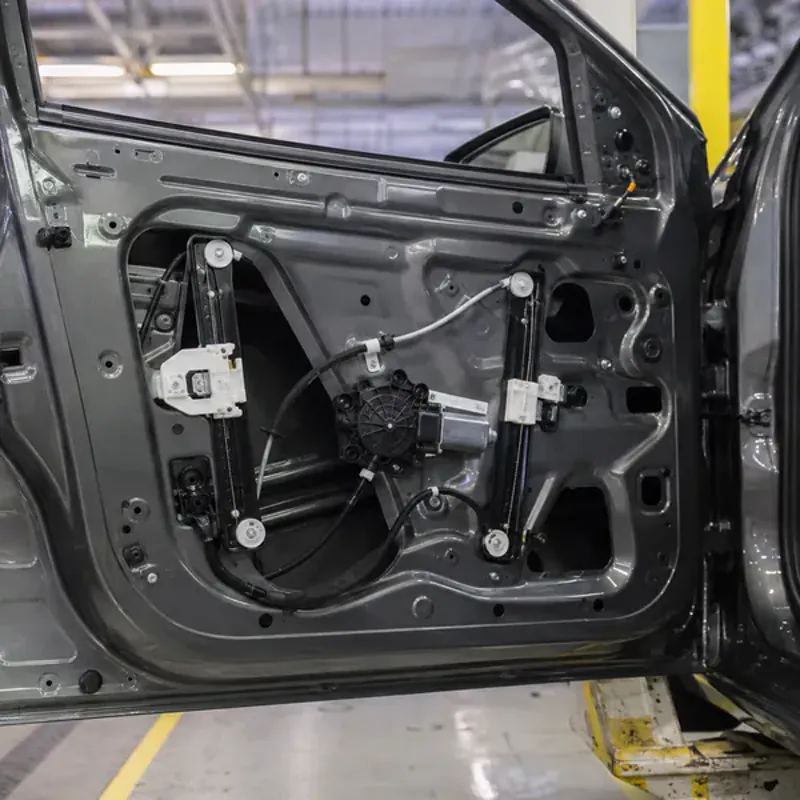
Automotive Motors Application

Automotive Motors

Automotive components must remain reliable across a wide temperature range, under vibration and over a long service life. GX rotors are used in:

  • Window-lift and seat-adjustment motors
  • HVAC air-flap and air-recirculation actuators
  • Electric power steering (EPS) motors
  • Sensor rotors for ABS and traction-control systems
  • Engine-cooling and radiator-fan motors
  • Fuel pumps and water pumps
  • Wiper motors and headlamp actuators

Typical rotor types: Injection-molded bonded ferrite rotors, injection-molded bonded NdFeB rotors and multipole sensor rings. Cabin applications may require operating temperatures of up to 150°C.

Home Appliance Motors Application

Home Appliance Motors

Home appliances require consistent performance at high production volumes, with cost efficiency and low noise as key priorities. GX is a qualified supplier to several major appliance manufacturers. Applications include:

  • Dishwasher circulation and drain pumps
  • Washing-machine drive motors and drain pumps
  • Refrigerator compressors and condenser fans
  • Indoor and outdoor air-conditioner fan motors
  • Vacuum cleaners and handheld vacuums
  • Blenders, food processors and coffee machines
  • Aquarium and water-circulation pumps
  • Ceiling and ventilation fans

Typical rotor types: Sintered ferrite multipole rings, injection-molded bonded ferrite rotors and axially magnetized ring magnets. Annual demand for a single part number can reach tens of millions of units.

Industrial Motors Application

Industrial Motors

Industrial applications range from low-power sensors to high-torque servo drives. Precision and durability are common requirements across the sector:

  • Industrial fans and blowers
  • Centrifugal and circulation pumps
  • Servo motors for CNC machines and automation
  • Stepper motors for positioning systems
  • Encoder and resolver magnet rings
  • Proximity switches and speed sensors
  • Conveyor and material-handling motors
  • Textile-machinery drives
  • Packaging and labeling-machine motors

Typical rotor types: Sintered NdFeB surface-mounted permanent-magnet (SPM) rotors for servo and high-torque applications; injection-molded bonded ferrite rotors for fans and pumps; and multipole encoder rings for precision position feedback.

Power Tool Motors Application

Power Tool Motors

Power tools require high power density, rapid acceleration and durability under intermittent heavy loads. Applications include:

  • Cordless and corded drills and drill drivers
  • Angle grinders and cut-off tools
  • Impact wrenches and rotary hammers
  • Jigsaws, circular saws and reciprocating saws
  • Sanders and polishers
  • Electric screwdrivers and nut runners
  • Garden tools, including lawn mowers, hedge trimmers and leaf blowers
  • Electric pruning shears and string trimmers

Typical rotor types: Sintered NdFeB SPM rotors for high power density, with high-coercivity SH or UH grades for elevated-temperature conditions. Rotors are dynamically balanced to grade G2.5 for smooth high-speed operation.

FAQ

Permanent-Magnet Rotor Assembly Sourcing Questions

Answers to the rotor-type, drawing, material, interface and validation questions buyers normally resolve before selecting a product route.

Which permanent-magnet rotor types can GX review?

GX can review drawing-defined rotor projects for PMSMs, BLDC motors, permanent-magnet stepper motors, permanent-magnet generators and PM-assisted synchronous reluctance motors. Final feasibility and supply scope depend on the approved drawings, BOM and validation requirements.

What is the difference between a BLDC rotor and a PMSM rotor?

Both use permanent magnets, and their physical structures may overlap. The distinction normally comes from the motor's back-EMF target, winding and control strategy. Pole arc, magnet topology, waveform, sensor alignment and torque-ripple requirements must therefore be reviewed with the mating stator and controller.

Can GX review both SPM and IPM rotor structures?

SPM and IPM projects can be evaluated from the complete rotor drawing. The review covers magnet geometry and position, rotor-core features, retention, air-gap surfaces, operating speed and the magnetic or mechanical acceptance criteria specified for the project.

Can ferrite, sintered NdFeB or bonded magnets be used in the rotor?

These magnet systems can be reviewed where appropriate, but they are not interchangeable. Magnet geometry, available magnetic output, temperature behavior, corrosion protection, magnetization, retention and rotor space must match the specific machine design.

Which components can be included in the rotor assembly?

The reviewed scope may include the rotor core, permanent magnets, shaft, hub, sleeve and retention parts. Bearings, fans, sensor targets or other components are included only when listed in the approved BOM and drawings.

Can dynamic balancing and overspeed validation be included?

These items can be reviewed when the buyer defines the operating and test speeds, balance grade or residual-unbalance limit, correction planes, measurement datum, overspeed condition and required report.

How are magnetic output and pole position verified?

Acceptance may use magnetic flux, surface flux-density waveform, pole count, pole sequence, circumferential pole position or another agreed functional characteristic. The fixture, air gap, measurement position, magnetization state and test condition must be defined.

What should be included in a permanent-magnet rotor RFQ?

Provide the assembly and component drawings, BOM, machine type, mating-stator information, magnet specification, pole map, critical fits and datums, retention method, speed, balance, environment, sample quantity and annual demand.

Request for quotation

Request a Permanent-Magnet Rotor Review

Identify the machine type and include the drawings, BOM, magnet system, mating interfaces, operating conditions and required validation.

  • PMSM, BLDC, PM stepper, PM generator
  • Rotor core, magnets, shaft, hub, sleeve and complete BOM
  • Pole layout, magnetization, fits, retention and torque-transfer interfaces
  • TIR, balance, rated and maximum speed, temperature and environment

Supported formats: PDF, JPG, PNG                                                  

No file selected

By submitting this form, you agree to provide accurate project information for evaluation. Information is kept confidential.